
Exceptionally quiet operation
Special design and oil-lubricated operation ensure very low noise levels, making the pump suitable even for environments with stricter noise requirements.
Compact vacuum pump with integrated motor and very quiet running. The ultimate vacuum range can be selected according to process needs: fine vacuum down to 2 mbar (abs.) or rough vacuum down to 10 mbar (abs.).
| Operation: oil-flooded rotary vane vacuum pumps |
| Suction capacity: 10–18 m³/h |
| Ultimate pressure: 2 mbar (abs.) (fine vacuum) or 10 mbar (abs.) (rough vacuum) – user selectable |
| Operation: oil-flooded rotary vane vacuum pumps |
| Suction capacity: 10–18 m³/h |
| Ultimate pressure: 2 mbar (abs.) (fine vacuum) or 10 mbar (abs.) (rough vacuum) – user selectable |
| Parameter | V-VGD 10 | V-VGD 15 |
|---|---|---|
| Suction capacity [m³/h] | 10 | 15 |
| Ultimate pressure (fine / rough vacuum) [mbar (abs.)] | 2 / 10 | 2 / 10 |
| Motor version | 3~ 200–255 / 346–440 V ± 5 %; 1~ 230 V ± 10 % | 3~ 200–255 / 346–440 V ± 5 %; 1~ 230 V ± 10 % |
| Motor power (3~) [kW] | 0,37 | 0,55 |
| Motor power (1~) [kW] | 0,37 | 0,55 |
| Current (3~) (Δ / Y) [A] | 2,4 / 1,4 | 2,8 / 1,6 |
| Current (1~) [A] | 2,8 | 3,5 |
| Rotational speed [min⁻¹] | 2850 | 2850 |
| Average sound pressure level [dB(A)] | 59 | 60 |
| Maximum weight [kg] | 19 | 19 |
| Oil capacity [l] | 0,4 | 0,4 |
Special design and oil-lubricated operation ensure very low noise levels, making the pump suitable even for environments with stricter noise requirements.
Single-side supported rotor and integrated motor enable very small outer dimensions and easy integration into machines and systems.
Users can choose between fine vacuum down to 2 mbar (abs.) or rough vacuum down to 10 mbar (abs.), enabling optimal adaptation to different processes.
Integrated high-efficiency oil separator and fine suction filter ensure that exhaust air remains virtually free of oil aerosols under all operating conditions.
Standard-integrated non-return valve, fine suction filter, and oil separator allow fast servicing and high equipment availability.
Suitable for use in woodworking, general industry, environmental technology, packaging systems, and pneumatic conveying.

Oil-lubricated rotary vane vacuum pumps are a standard solution for packaging machines, chamber packers, and central vacuum systems where reliable rough or fine vacuum and continuous operation are required.
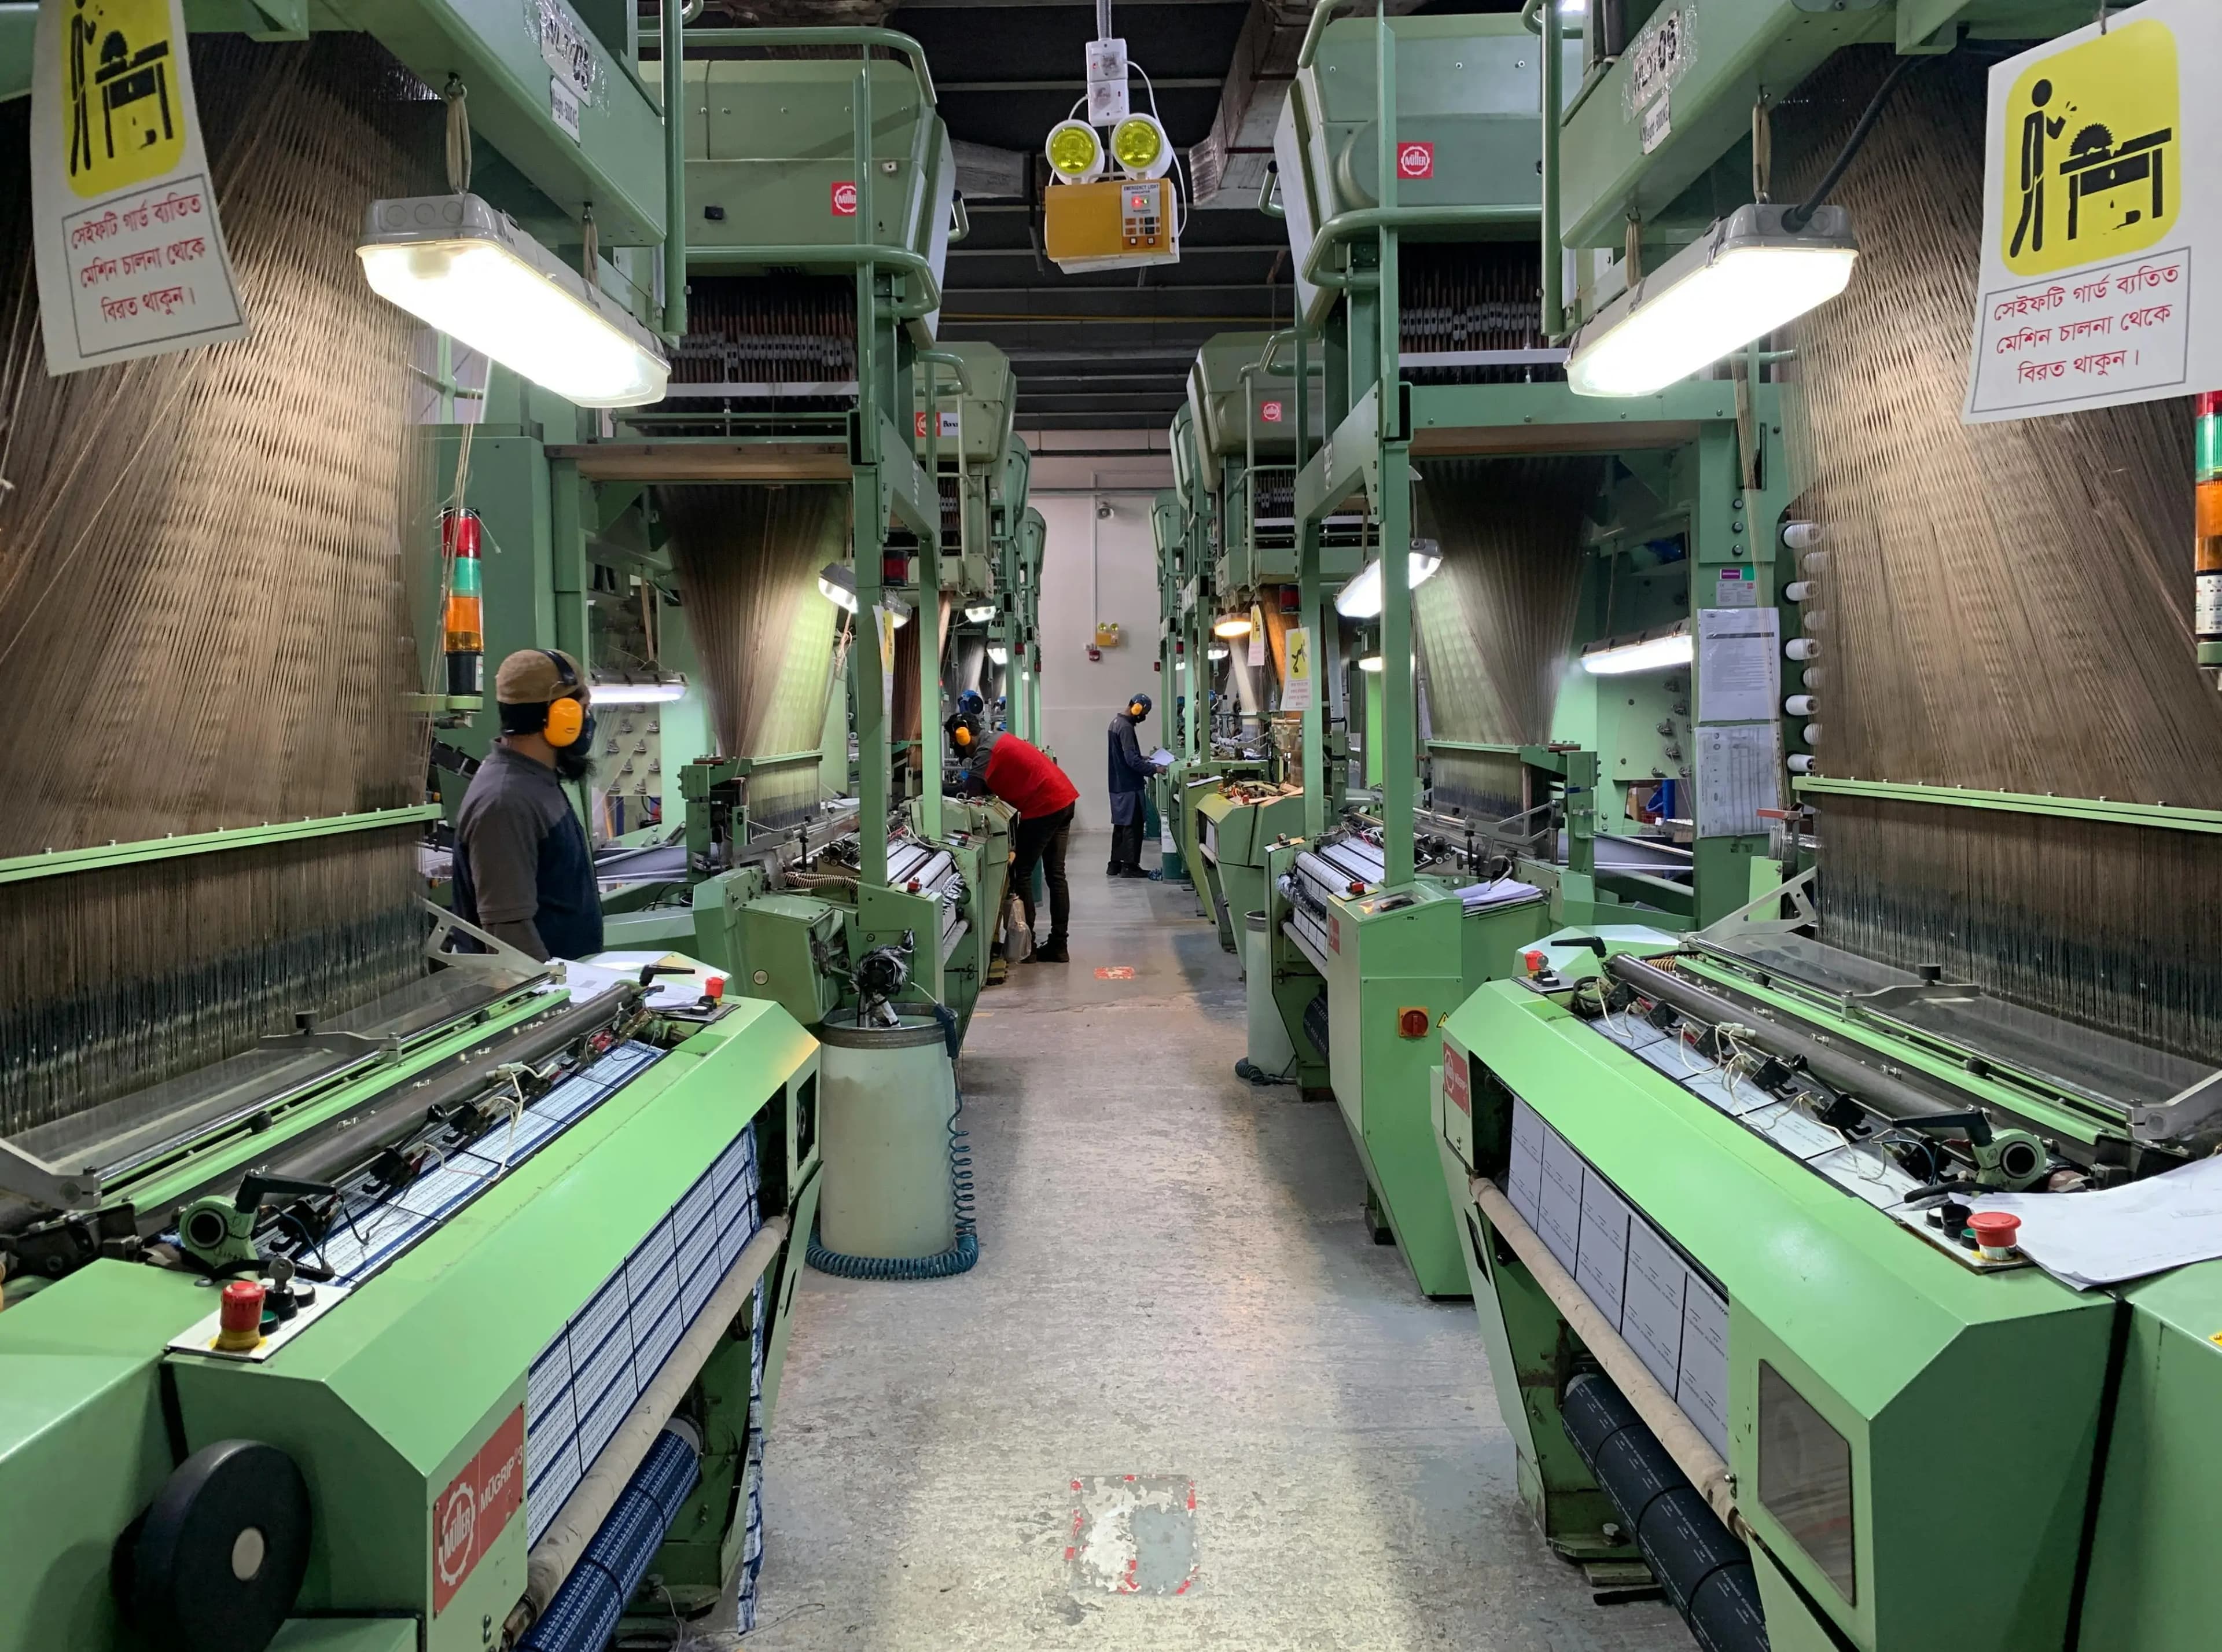
Used across a wide range of industrial processes such as clamping, handling, extraction, and central vacuum systems. Oil-lubricated rotary vane pumps provide stable vacuum and long service life.

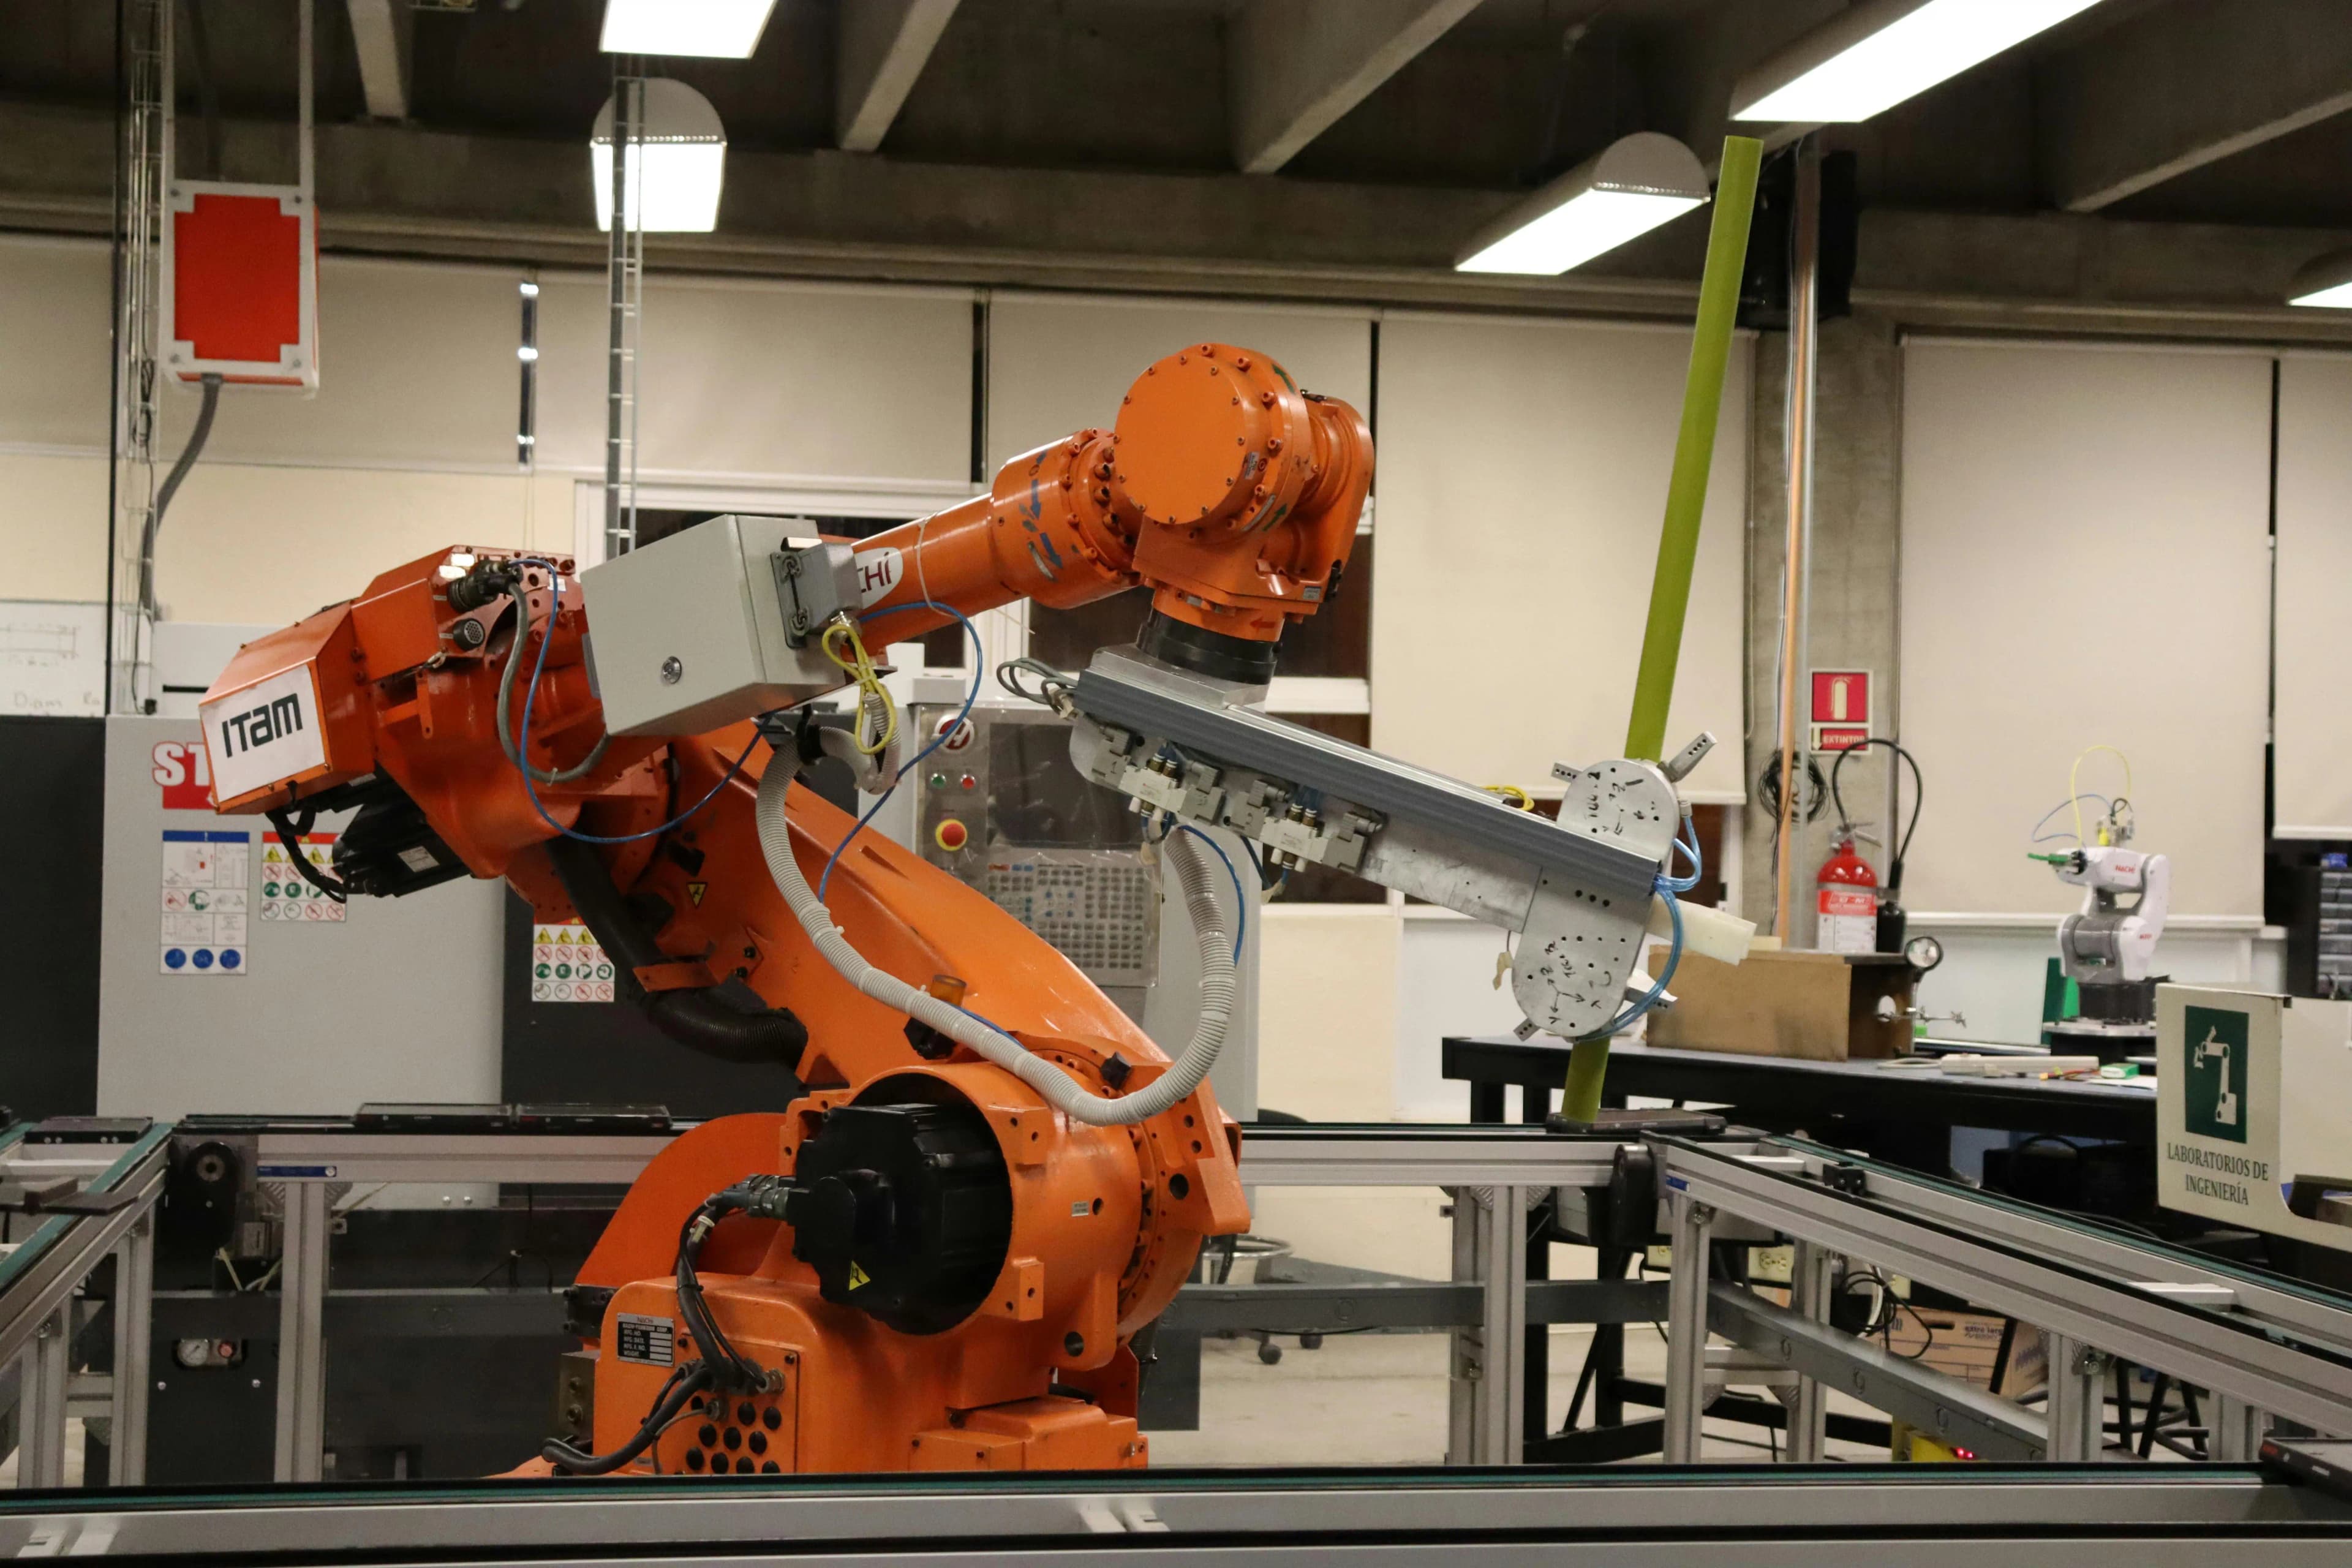
Suitable for vacuum clamping of workpieces, CNC tables, and extraction systems. Oil-lubricated rotary vane vacuum pumps are valued for quiet running, robustness, and reliable continuous operation.
Used in pneumatic conveying of bulk materials and dust where moderate to deep vacuum and reliable continuous operation in industrial environments are required.

Suitable for central industrial vacuum stations where multiple consumers require stable vacuum. Oil-lubricated rotary vane pumps enable reliable and economical long-term operation.
Fill in a short form and we will prepare a proposal for a vacuum pump or blower based on flow, pressure, and operating conditions. If needed, we can also include filtration, silencers, and accessories.
Explore other vacuum and blower solutions from Elmo Rietschle.
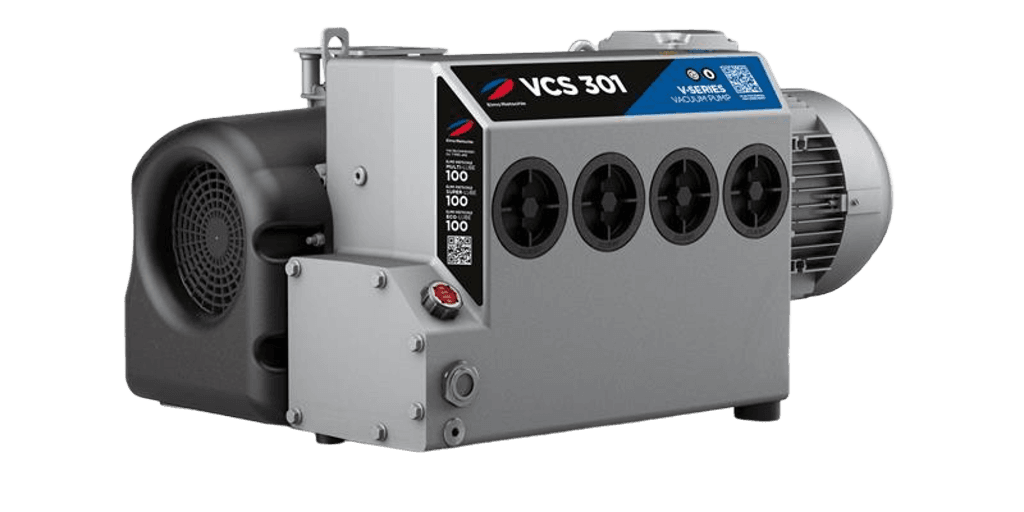
Advanced new-generation oil-lubricated rotary vane vacuum pump with optimized energy consumption, low noise and reduced maintenance costs. The compact design allows easy integration into OEM equipment and retrofitting of existing systems. Suction capacity 40–360 m³/h (up to 1500 m³/h for larger models), ultimate vacuum up to 0.5 mbar (abs.).
More about the device→
Oil-lubricated rotary vane vacuum pump for demanding applications with moisture and vapor, equipped with resistant vanes and an enlarged gas ballast valve.
More about the device→
Oil-lubricated rotary vane vacuum pump with integrated motor and single-side rotor bearing support. Small footprint, air cooling, and very quiet running. Suction capacity 4–7.2 m³/h, ultimate vacuum up to 20 mbar (abs.).
More about the device→
Industrial oil-lubricated rotary vane vacuum pump with flange-mounted motor and double-side supported rotor. Designed for reliable continuous duty. Suction capacity 25–48 m³/h, ultimate vacuum up to 10 mbar (abs.).
More about the device→
Compact oil-lubricated rotary vane vacuum pump with integrated motor and single-side rotor bearing support. Designed for fine vacuum at lower flow rates. Suction capacity 4–7.2 m³/h, ultimate vacuum up to 2 mbar (abs.).
More about the device→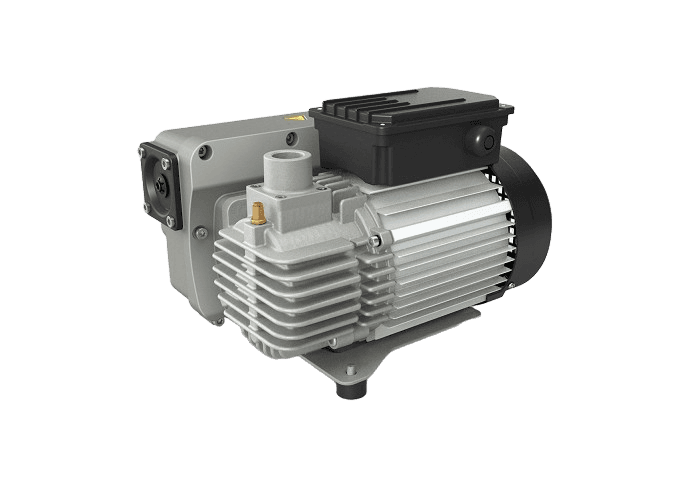
Oil-lubricated rotary vane vacuum pump with integrated motor and single-side rotor bearing support. User-selectable ultimate vacuum: fine vacuum 2 mbar (abs.) or rough vacuum 10 mbar (abs.). Suction capacity 10–18 m³/h.
More about the device→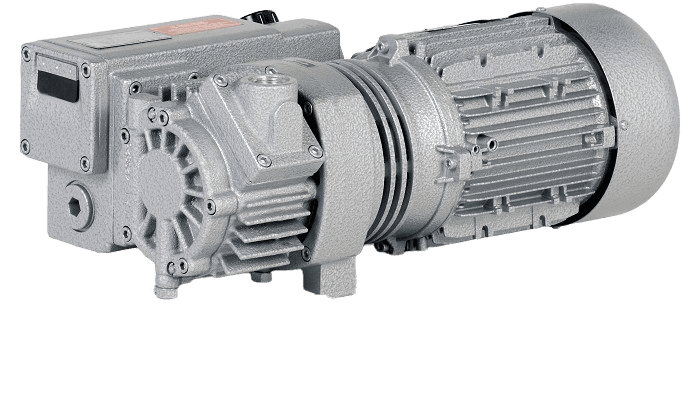
Oil-lubricated rotary vane vacuum pump for smaller chamber packaging machines. Flange-mounted motor and double-side supported rotor ensure stable operation. Suction capacity 20–26.5 m³/h, ultimate vacuum up to 2 mbar (abs.).
More about the device→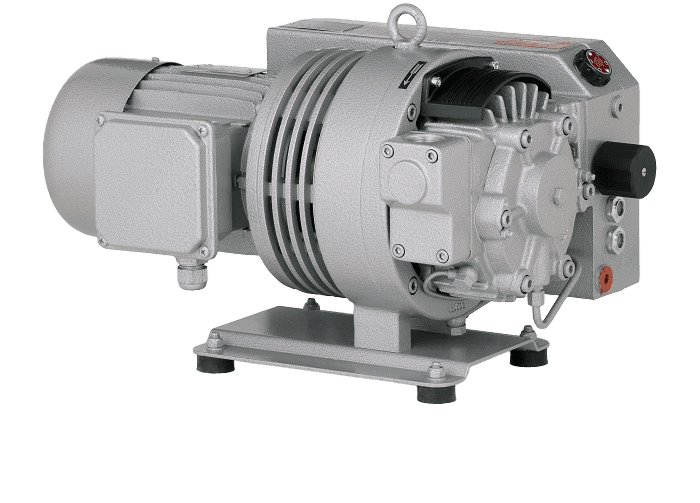
Industrial oil-lubricated rotary vane vacuum pump with dual rotor bearing support and flange-mounted motor. Suitable for applications requiring deeper vacuum. Suction capacity 25–48 m³/h, ultimate vacuum up to 0.5 mbar (abs.).
More about the device→
High-capacity oil-lubricated rotary vane vacuum pump for demanding industrial processes and central vacuum systems. Available across a very wide size range. Suction capacity 50–1,535 m³/h, ultimate vacuum up to 0.1 mbar (abs.).
More about the device→